Introduction
Efficient flow control is essential for every industrial process, whether it involves transporting liquids, gases, steam, chemicals, or compressed air. From oil refineries and petrochemical plants to pharmaceutical facilities and water treatment systems, industrial valves ensure safe operation, accurate flow regulation, and dependable process control.
Among the different types of industrial valves available, Ball Valves have become one of the most widely used solutions because of their simple design, quick operation, leak-tight sealing, and exceptional durability.
Mcneil Air Header manufactures, supplies, and exports high-performance Industrial Ball Valves designed for demanding applications where reliability, pressure resistance, and long service life are critical. The company offers precision-engineered ball valves for instrumentation, process piping, hydraulic systems, and industrial flow control applications.
What Is a Ball Valve?
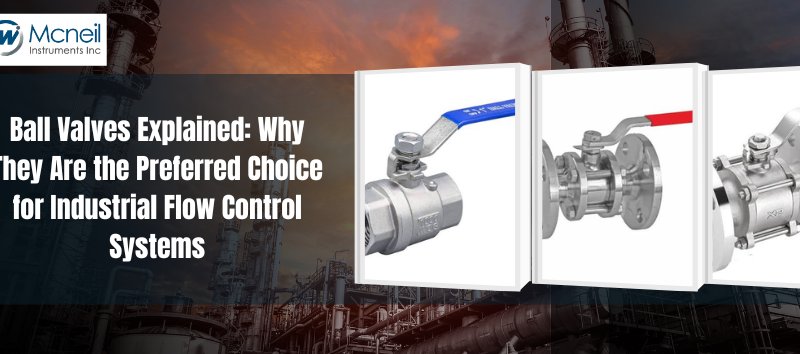
A Ball Valve is a quarter-turn valve that uses a precision-machined spherical ball with a central bore to control the flow of fluids or gases.
When the bore aligns with the pipeline, the valve remains open.
When rotated 90 degrees, the solid portion of the ball blocks the flow completely, providing reliable shut-off.
Because of this simple operating mechanism, Ball Valves are widely preferred for fast, efficient, and leak-proof flow control.
Why Ball Valves Are Widely Used
Industrial facilities choose Ball Valves because they provide:
• Quick quarter-turn operation
• Bubble-tight shut-off
• Low pressure drop
• Excellent sealing performance
• High-pressure capability
• Long operational life
• Easy maintenance
• Reliable performance in demanding environments
These advantages make Ball Valves suitable for both manual and automated industrial systems.
Mcneil Air Header – Trusted Ball Valve Manufacturer
Mcneil Air Header manufactures precision-engineered Ball Valves for industrial and instrumentation applications.
The product portfolio includes:
• Stainless Steel Ball Valves
• Carbon Steel Ball Valves
• Alloy Steel Ball Valves
• Two-Way Ball Valves
• Three-Way Ball Valves
• High Pressure Ball Valves
• Instrumentation Ball Valves
• Panel Mount Ball Valves
• Threaded Ball Valves
• Socket Weld Ball Valves
• Flanged Ball Valves
Each valve is manufactured to deliver dependable sealing performance, smooth operation, and long service life in demanding industrial environments.
Types of Ball Valves
Two-Way Ball Valves
The most commonly used design for on/off flow control.
Applications
• Process Pipelines
• Water Systems
• Oil & Gas
• Chemical Plants
Three-Way Ball Valves
Designed to divert or mix flow between multiple pipeline directions.
Benefits
• Flow diversion
• Compact installation
• Reduced piping complexity
High Pressure Ball Valves
Engineered for systems operating under elevated pressure conditions.
Advantages
• Excellent pressure resistance
• Leak-proof sealing
• High mechanical strength
Instrumentation Ball Valves
Used for precise isolation in instrumentation and control systems.
Applications
• Pressure Transmitters
• Instrument Panels
• Pneumatic Systems
• Hydraulic Systems
Materials Used in Ball Valve Manufacturing
Mcneil Air Header manufactures Ball Valves using premium industrial materials.
Stainless Steel Ball Valves
Available Grades
• SS 304 Ball Valves
• SS 316 Ball Valves
Benefits
• Excellent corrosion resistance
• Hygienic surface finish
• Long service life
Ideal for:
• Chemical Processing
• Pharmaceutical Plants
• Food Industries
• Marine Applications
Carbon Steel Ball Valves
Designed for general industrial service.
Advantages
• High mechanical strength
• Cost-effective
• Excellent pressure capability
Alloy Steel Ball Valves
Available in:
• ASTM A182 F5 Ball Valves
• ASTM A182 F11 Ball Valves
• ASTM A182 F22 Ball Valves
• ASTM A182 F91 Ball Valves
Suitable for:
• High-temperature systems
• Steam service
• Refineries
• Power plants
Exotic Alloy Ball Valves
Mcneil Air Header also manufactures Ball Valves in premium alloys including:
• Monel Ball Valves
• Inconel Ball Valves
• Incoloy Ball Valves
• Hastelloy Ball Valves
These materials are ideal for aggressive chemical processing, offshore installations, and highly corrosive environments.
Key Advantages of Ball Valves
Fast Operation
Quarter-turn design allows quick opening and closing.
Leak-Proof Performance
Precision-machined seats provide reliable shut-off.
Low Flow Resistance
The full-port design minimizes pressure drop and maximizes flow efficiency.
High Durability
Ball Valves perform reliably even after thousands of operating cycles.
Minimal Maintenance
Simple internal construction reduces wear and servicing requirements.
Industries Using Ball Valves
Oil & Gas
Used in:
• Refineries
• Pipelines
• Offshore Platforms
Petrochemical Industry
Supports:
• Chemical Transfer Systems
• Process Piping
• Instrumentation
Power Generation
Installed in:
• Boilers
• Steam Systems
• Cooling Water Networks
Chemical Processing
Provides reliable isolation for corrosive process fluids.
Water Treatment
Used in filtration systems, pumping stations, and distribution pipelines.
Pharmaceutical Industry
Suitable for hygienic and contamination-sensitive applications.
Marine Industry
Offers dependable flow control for shipbuilding and offshore installations.
Mcneil Air Header manufactures industrial ball valves for oil & gas, petrochemical, power generation, chemical processing, marine, and instrumentation applications.
Technical Specifications
| Parameter | Specification |
| Product | Industrial Ball Valve |
| Types | Two-Way, Three-Way, High Pressure, Instrumentation |
| Materials | Stainless Steel, Carbon Steel, Alloy Steel, Monel, Inconel, Hastelloy, Incoloy |
| End Connections | Threaded, Socket Weld, Flanged |
| Applications | Oil & Gas, Petrochemical, Power, Chemical, Marine |
Quality Assurance
Every Ball Valve manufactured by Mcneil Air Header undergoes comprehensive quality inspections including:
• Hydrostatic Testing
• Pneumatic Testing
• Pressure Testing
• PMI Testing
• Leak Testing
• Dimensional Inspection
• Material Traceability Verification
• Visual Inspection
These testing procedures ensure every valve meets international quality standards before delivery.
Why Choose Mcneil Air Header?
Industries worldwide trust Mcneil Air Header because of:
• Precision-engineered Ball Valves
• Premium-grade materials
• International manufacturing standards
• High-pressure valve expertise
• Custom valve configurations
• Strict quality control
• Global export capability
• Technical engineering support
The company supplies dependable valve solutions that improve operational safety, process efficiency, and long-term system reliability.
Conclusion
Ball Valves have become an essential component in modern industrial piping systems because they combine simple operation with outstanding sealing performance, high durability, and low maintenance requirements.
Whether your application requires Stainless Steel Ball Valves, Carbon Steel Ball Valves, Alloy Steel Ball Valves, Two-Way Ball Valves, Three-Way Ball Valves, High Pressure Ball Valves, Instrumentation Ball Valves, Threaded Ball Valves, Socket Weld Ball Valves, or Flanged Ball Valves, Mcneil Air Header delivers precision-engineered valve solutions designed to perform in the world’s most demanding industrial environments.