Introduction
Modern industrial facilities depend on precise flow control to ensure the safe and efficient operation of instrumentation systems, process equipment, pneumatic controls, hydraulic systems, and automation networks. Ball Valves and Needle Valves are essential components that regulate, isolate, and control the flow of liquids, gases, steam, and other industrial media with exceptional accuracy and reliability.
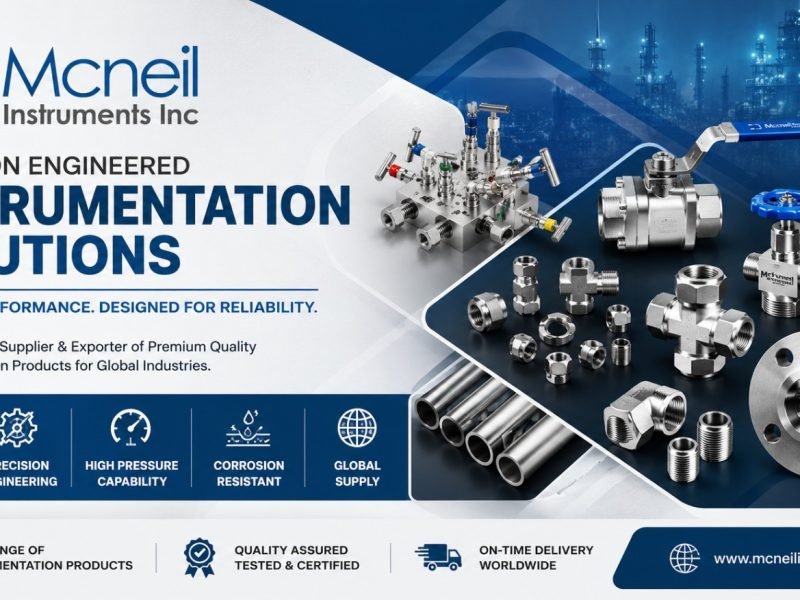
Mcneil Air Header is a leading manufacturer, supplier, and exporter of premium-quality Ball Valves and Needle Valves, engineered for demanding industrial applications. Manufactured using high-quality Stainless Steel, Carbon Steel, Alloy Steel, Duplex Stainless Steel, Super Duplex Steel, Monel, Hastelloy, and Inconel, our valves deliver superior corrosion resistance, leak-proof sealing, and long service life.
Our precision-engineered industrial valves are trusted across oil & gas, petrochemical, chemical processing, power generation, marine, pharmaceutical, water treatment, and industrial automation industries worldwide.
Why Choose Mcneil Air Header for Ball Valves & Needle Valves?
Choosing the right industrial valve manufacturer ensures dependable performance, process safety, and long-term operational efficiency.
Why Customers Trust Us
✔ Premium-quality raw materials
✔ Precision-engineered valves
✔ Leak-proof sealing performance
✔ Corrosion-resistant materials
✔ High-pressure capability
✔ International quality standards
✔ Custom sizes and end connections
✔ Competitive pricing
✔ Fast worldwide delivery
✔ Dedicated technical support
Our Ball Valves and Needle Valves are manufactured according to international quality standards to provide consistent performance in critical industrial environments.
What are Ball Valves & Needle Valves?
Ball Valves
A Ball Valve is a quarter-turn valve that uses a rotating ball with a bore to quickly start or stop the flow of fluids. Ball Valves are known for their excellent sealing capability, minimal pressure loss, and reliable operation.
Features
- Quarter-turn operation
- Bubble-tight shut-off
- Low pressure drop
- High durability
- Excellent corrosion resistance
- Easy maintenance
- Long service life
Applications
- Process plants
- Oil & Gas pipelines
- Water treatment systems
- Chemical processing
- Marine applications
- Industrial automation
Needle Valves
A Needle Valve is a precision flow control valve designed with a tapered needle-like plunger that allows accurate regulation of fluid flow and pressure.
Features
- Precise flow adjustment
- Excellent pressure control
- Leak-proof sealing
- Smooth operation
- High-pressure capability
- Compact design
- Long operational life
Applications
- Instrumentation systems
- Hydraulic systems
- Pneumatic systems
- Pressure gauge isolation
- Sampling systems
- Laboratory applications
Our Range of Ball Valves & Needle Valves
Ball Valves
Mcneil Air Header manufactures premium Ball Valves suitable for various industrial applications.
Product Features
- Full Port Ball Valves
- Reduced Port Ball Valves
- High Pressure Ball Valves
- Instrumentation Ball Valves
- Two Way Ball Valves
- Three Way Ball Valves
- Screwed End Ball Valves
- Socket Weld Ball Valves
- Butt Weld Ball Valves
- Flanged Ball Valves
Applications
- Oil & Gas
- Chemical Plants
- Refineries
- Water Treatment
- Power Plants
- Industrial Pipelines
Needle Valves
Our precision Needle Valves provide superior flow control for instrumentation and pressure regulation.
Product Features
- Instrumentation Needle Valves
- High Pressure Needle Valves
- Straight Pattern Needle Valves
- Angle Pattern Needle Valves
- Panel Mount Needle Valves
- Integral Bonnet Needle Valves
Applications
- Instrument Air Systems
- Hydraulic Equipment
- Pneumatic Systems
- Chemical Processing
- Pressure Measurement
- Process Control
Benefits of Ball Valves & Needle Valves in Industrial Instrumentation Systems
Installing premium-quality industrial valves improves plant efficiency, operational safety, and long-term reliability.
Key Benefits
✔ Reliable flow isolation
✔ Accurate flow regulation
✔ Leak-proof operation
✔ Improved plant safety
✔ High-pressure performance
✔ Reduced maintenance costs
✔ Longer equipment life
✔ Corrosion resistance
✔ Easy installation
✔ Improved process efficiency
Types of Industrial Valves We Manufacture
Mcneil Air Header manufactures a comprehensive range of industrial valves.
Product Range
- Ball Valves
- Needle Valves
- Instrumentation Ball Valves
- Instrumentation Needle Valves
- High Pressure Ball Valves
- High Pressure Needle Valves
- Two Way Ball Valves
- Three Way Ball Valves
- Screwed End Valves
- Socket Weld Valves
- Butt Weld Valves
- Flanged Valves
- Customized Industrial Valves
Available with threaded, socket weld, butt weld, and flanged end connections.
Available Material Grades
Our Ball Valves and Needle Valves are manufactured using premium industrial materials suitable for demanding applications.
Material Options
- Stainless Steel 304
- Stainless Steel 304L
- Stainless Steel 316
- Stainless Steel 316L
- Carbon Steel
- Alloy Steel
- Duplex Stainless Steel
- Super Duplex Stainless Steel
- Monel
- Hastelloy
- Inconel
- Brass
Custom material grades are available upon request.
Industries We Serve
Our Ball Valves and Needle Valves are widely used across numerous industrial sectors.
Major Industries
- Oil & Gas
- Petrochemical Plants
- Chemical Processing
- Refineries
- Power Generation
- Marine & Offshore
- Pharmaceutical Industry
- Water Treatment Plants
- Food Processing
- Fertilizer Plants
- Steel Plants
- Industrial Automation
- LNG Plants
- Process Equipment Manufacturing
International Standards
Our industrial valves are manufactured in compliance with internationally recognized standards.
Available Standards
- ASME
- ANSI
- ASTM
- API
- ISO
- DIN
- EN
- MSS
- NACE
Available in multiple pressure ratings, sizes, end connections, and customized specifications.
Why Industries Prefer Mcneil Air Header Valves
Our Ball Valves and Needle Valves help improve plant performance while reducing operational costs.
Business Advantages
🌍 Reliable flow control
⚙ Precision operation
🛡 Leak-proof sealing
📈 Improved equipment reliability
💰 Reduced maintenance costs
🚀 Lower plant downtime
📊 Enhanced operational safety
🔧 Long service life
Quality Assurance at Mcneil Air Header
Every industrial valve undergoes rigorous quality inspection before dispatch.
Quality Checks Include
- Raw Material Verification
- PMI Testing
- Hydrostatic Pressure Testing
- Pneumatic Leak Testing
- Pressure Testing
- Dimensional Inspection
- Thread Inspection
- Surface Finish Inspection
- Visual Inspection
- Material Traceability
Material Test Certificates (MTC) and inspection reports are available upon request.
Why Customers Choose Mcneil Air Header
Industrial customers worldwide trust Mcneil Air Header for premium-quality industrial valves.
Our Strengths
✔ Premium quality products
✔ Large ready inventory
✔ Precision manufacturing
✔ Competitive pricing
✔ Fast international delivery
✔ Technical assistance
✔ Custom manufacturing
✔ Reliable customer support
Benefits of Choosing Our Ball Valves & Needle Valves
Partnering with Mcneil Air Header provides long-term operational advantages.
📊 Reliable industrial performance
🌍 Global supply capability
⚙ Precision-engineered valves
🛠 Long-lasting durability
📈 Improved plant efficiency
💼 Trusted manufacturing expertise
📞 Contact Mcneil Air Header Today
Looking for premium-quality Ball Valves and Needle Valves for your industrial instrumentation or process control systems?
Mcneil Air Header
📧 info@mcneilinstruments.com
📞 +91 9870883613
Our experts are ready to assist you with product selection, technical specifications, pricing, bulk orders, and customized valve solutions.
Frequently Asked Questions (FAQs)
1. What is the difference between Ball Valves and Needle Valves?
Ball Valves are designed for quick on/off flow isolation, while Needle Valves provide precise flow regulation and pressure control in instrumentation systems.
2. What are the advantages of using Ball Valves and Needle Valves?
They provide leak-proof sealing, accurate flow control, corrosion resistance, high-pressure capability, long service life, and reduced maintenance.
3. Which industries commonly use Ball Valves and Needle Valves?
They are widely used in oil & gas, petrochemical, chemical processing, power generation, pharmaceutical, marine, water treatment, instrumentation, hydraulic, and pneumatic systems.
4. Which materials are available for your industrial valves?
Our valves are manufactured in Stainless Steel, Carbon Steel, Alloy Steel, Duplex Steel, Super Duplex Steel, Monel, Hastelloy, Inconel, and Brass.
5. Do you manufacture customized Ball Valves and Needle Valves?
Yes. We manufacture customized industrial valves in various sizes, pressure ratings, end connections, and material grades according to customer requirements.
6. Why choose Mcneil Air Header?
Mcneil Air Header offers precision-engineered industrial valves, premium materials, strict quality testing, customized manufacturing, competitive pricing, worldwide exports, and reliable technical support.