Introduction: Controlling Condensation Is Not Optional
Here’s the thing—steam systems don’t just carry steam, they carry moisture, pressure fluctuations, and thermal stress. If condensate isn’t handled properly, it leads to inaccurate readings, equipment damage, and system inefficiency.
That’s where a condensate pot becomes critical. It collects and holds condensate before it reaches sensitive instruments, ensuring accurate pressure measurement and system stability.
As a trusted condensate pot manufacturer in India, the focus is on reliability, compliance, and performance—especially when delivering IBR condensate pot and seal pot supplier for steam systems solutions.
What Is a Condensate Pot?
A condensate pot is a device installed in steam lines to collect and store condensate, preventing it from entering pressure instruments.
It acts as a protective barrier between steam and instrumentation.
Key Functions
- Prevents direct contact of steam with instruments
• Maintains equal liquid column for accurate readings
• Protects transmitters and gauges
• Improves system safety and efficiency
What this really means is simple: stable readings and longer equipment life.
What Is a Seal Pot in Steam Systems?
A seal pot supplier for steam systems provides specialized pots used to maintain a constant liquid seal in pressure measurement lines.
Seal pots are essential in differential pressure applications where accuracy matters.
Why Seal Pots Matter
- Maintains consistent hydrostatic pressure
• Prevents steam from entering impulse lines
• Ensures accurate differential pressure readings
• Reduces instrument damage
Why IBR Condensate Pot Is Important
When dealing with boilers and high-pressure steam, compliance is non-negotiable.
An IBR condensate pot manufacturer ensures products meet Indian Boiler Regulations (IBR) standards.
Benefits of IBR Condensate Pots
- Certified for high-pressure steam applications
• Ensures safety and regulatory compliance
• Suitable for boiler and power plant systems
• Built for extreme pressure and temperature conditions
This is why industries prefer an IBR condensate pot manufacturer for critical operations.
Key Features of Condensate Pots
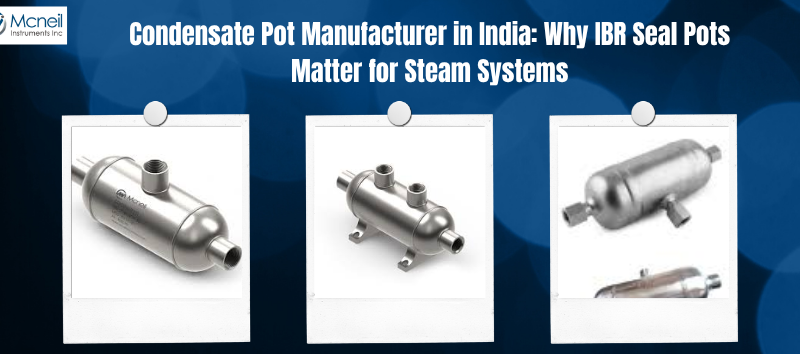
A well-designed condensate pot includes:
- Inlet and outlet connections
• Drain valve for condensate removal
• Vent connection for air release
• Robust cylindrical construction
• Mounting support for installation
These features ensure efficient condensate handling and system protection.
Technical Specifications of Condensate Pots
| Parameter | Details |
| Material | SS304 / SS316 / Carbon Steel |
| Size Range | ½” to 4” |
| Pressure Rating | Up to 6000 PSI |
| End Connection | Threaded / Flanged |
| Orientation | Vertical / Horizontal |
| Finish | Polished / Coated |
Specifications can be customized based on steam system requirements.
Applications of Condensate Pots and Seal Pots
These components are widely used in steam and pressure systems.
Power Plants
Used in boiler systems and steam lines for pressure measurement.
Oil & Gas Industry
Ensures accurate pressure readings in high-temperature pipelines.
Chemical Industry
Handles aggressive fluids and steam-based processes.
Pharmaceutical Industry
Maintains clean and controlled steam systems.
Process Industries
Supports instrumentation in high-pressure environments.
Advantages of Choosing a Reliable Condensate Pot Manufacturer in India
Working with a trusted condensate pot manufacturer in India offers:
Precision Manufacturing
Ensures consistent performance in critical systems.
IBR Compliance
Meets mandatory safety and regulatory standards.
Custom Design Capability
Built according to pressure, size, and orientation requirements.
Cost-Effective Solutions
Competitive pricing with high durability.
Types of Condensate Pots
Stainless Steel Condensate Pot
- Corrosion-resistant
• Ideal for harsh and chemical environments
Carbon Steel Condensate Pot
- Economical option
• Suitable for general applications
IBR Condensate Pot
- Certified for boiler applications
• Designed for high-pressure steam systems
Seal Pots
- Used in differential pressure systems
• Maintains liquid seal for accuracy
Quality Testing of Condensate Pots
Every IBR condensate pot and seal pot undergoes strict testing:
- Hydrostatic pressure testing
• Leak testing
• Dimensional inspection
• Material traceability checks
• Surface and weld quality testing
This ensures safety, durability, and compliance.
How to Choose the Right Seal Pot Supplier for Steam Systems
Choosing the right seal pot supplier for steam systems matters.
What to Look For
- Experience in steam and boiler applications
• IBR certification capability
• High-grade raw materials (SS316 preferred)
• Custom manufacturing support
• Strong quality assurance
A reliable supplier ensures accurate readings and long-term performance.
Conclusion
A condensate pot is not just a component—it’s a critical safeguard for steam systems and instrumentation accuracy.
Choosing a reliable condensate pot manufacturer in India, a trusted seal pot supplier for steam systems, and an experienced IBR condensate pot manufacturer ensures safety, efficiency, and compliance.
If the goal is accurate pressure measurement, reduced equipment damage, and long-term reliability, investing in high-quality condensate and seal pots is the right decision.