Introduction
In industries where precision is critical, even the smallest variation in fluid or gas flow can impact system performance, product quality, and operational safety. From oil & gas facilities and petrochemical plants to power generation stations, pharmaceutical manufacturing units, and chemical processing facilities, accurate flow control remains one of the most important aspects of industrial operations.
This is where Needle Valves play a crucial role.
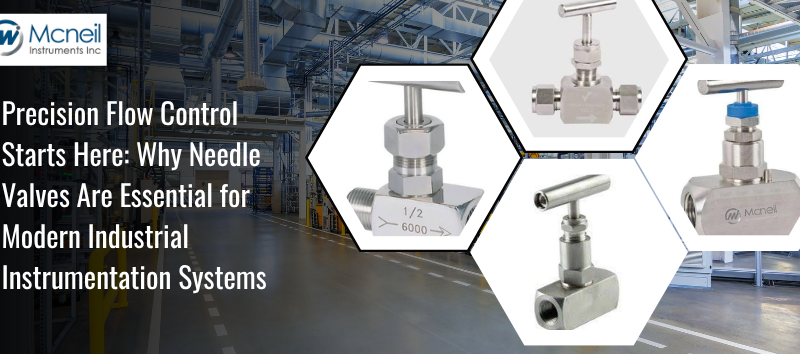
Designed for precise flow regulation, throttling, and shut-off applications, Needle Valves provide operators with exceptional control over fluid and gas movement. Their ability to deliver accurate flow adjustment, leak-tight sealing, and reliable performance under high-pressure conditions makes them one of the most widely used instrumentation valves across industrial sectors.
At Mcneil Air Header, Needle Valves are engineered to meet demanding industrial requirements, offering precision flow control solutions for critical applications worldwide.
What Is a Needle Valve?
A Needle Valve is a specialized flow control valve designed to regulate fluid or gas flow with exceptional accuracy.
Unlike conventional valves that primarily provide on-off control, Needle Valves use a finely tapered stem that gradually opens or closes the flow path, allowing operators to make highly precise flow adjustments. This design makes them ideal for applications requiring accurate metering and controlled flow regulation.
Needle Valves are commonly used in:
• Instrumentation Systems
• Hydraulic Systems
• Pneumatic Systems
• Process Control Applications
• Gas Distribution Networks
• Chemical Processing Systems
• Pressure Measurement Installations
Why Industries Depend on Needle Valves
Modern industrial systems require components capable of maintaining accuracy, reliability, and safety under challenging operating conditions.
Needle Valves provide:
• Precise flow regulation
• Bubble-tight shut-off capability
• Excellent pressure handling performance
• Long service life
• Leak-free sealing
• Reduced maintenance requirements
• High operational reliability
These advantages make Needle Valves a preferred choice for critical industrial applications.
Mcneil Air Header: Trusted Needle Valve Manufacturer
Mcneil Air Header manufactures and supplies a wide range of industrial Needle Valves designed for precision flow control applications.
Available materials include:
• Stainless Steel 304 Needle Valves
• Stainless Steel 316 Needle Valves
• Carbon Steel Needle Valves
• Alloy Steel Needle Valves
• Inconel Needle Valves
• Monel Needle Valves
• Hastelloy Needle Valves
These valves are engineered to withstand high pressures, elevated temperatures, and corrosive environments.
Understanding Different Types of Needle Valves
Type N / UN Needle Valves
Reliable Isolation for High-Pressure Systems
These valves feature metal-to-metal sealing and are designed for demanding industrial environments.
Key Benefits
• Bubble-tight sealing
• High-pressure capability
• Long operational life
• Superior temperature resistance
Applications
• Instrumentation Systems
• Oil & Gas Facilities
• Chemical Plants
Type PV Needle Valves
High Flow Performance with Precise Control
The PV Series utilizes a regenerative soft seat design for improved sealing and flow performance.
Advantages
• High flow capacity
• Precise throttling capability
• Excellent shut-off performance
Applications
• Viscous Fluid Systems
• Process Industries
• Hydraulic Applications
Type AV Needle Valves
Compact Design for Directional Flow Control
The AV Series incorporates a 90-degree angle pattern for installations where space optimization is important.
Features
• Compact body design
• High-pressure sealing
• Easy installation
Applications
• Instrument Panels
• Pneumatic Systems
• Process Control Networks
Type OB Needle Valves
Reduced Pressure Drop for Improved Efficiency
The OB Series provides a nearly straight flow path, minimizing flow restrictions.
Benefits
• Lower pressure loss
• Improved flow efficiency
• User-friendly operation
Applications
• Heavy Fluids
• Industrial Processing Systems
• High Flow Networks
Type UN-V Needle Valves
Enhanced Performance Under Extreme Conditions
Designed for demanding pressure and temperature applications.
Advantages
• Superior sealing performance
• High durability
• Excellent reliability
Applications
• Petrochemical Plants
• Offshore Platforms
• Power Generation Facilities
Materials Used in Needle Valve Manufacturing
Stainless Steel Needle Valves
The most widely used material for industrial flow control.
Benefits
• Excellent corrosion resistance
• Long service life
• Superior mechanical strength
Applications
• Chemical Plants
• Offshore Installations
• Pharmaceutical Facilities
Carbon Steel Needle Valves
Provide excellent strength and cost-effective performance.
Applications
• Utility Systems
• General Industrial Services
• Process Plants
Inconel Needle Valves
Designed for extreme temperatures and corrosive environments.
Applications
• LNG Facilities
• Petrochemical Plants
• Offshore Systems
Monel Needle Valves
Ideal for marine and seawater applications.
Applications
• Marine Engineering
• Offshore Installations
• Desalination Plants
Hastelloy Needle Valves
Built for aggressive chemical environments.
Applications
• Acid Processing Plants
• Chemical Manufacturing Facilities
• Corrosion-Sensitive Systems
Industries That Rely on Needle Valves
Oil & Gas Industry
Used in:
• Refineries
• Pipeline Systems
• Offshore Platforms
• Gas Processing Facilities
Petrochemical Industry
Supports:
• Process Control Systems
• Chemical Transfer Networks
• Instrumentation Installations
Power Generation Industry
Used in:
• Steam Systems
• Turbine Installations
• Pressure Measurement Applications
Chemical Processing Industry
Provides reliable flow control for corrosive media.
Marine Industry
Ensures dependable operation in harsh offshore environments.
Pharmaceutical Industry
Supports high-purity fluid handling systems.
Technical Features of Mcneil Air Header Needle Valves
Mcneil Air Header Needle Valves are designed to deliver reliable performance under demanding conditions.
Key features include:
• One-piece body construction
• SS316 construction options
• High-pressure ratings up to 10,000 PSI
• Precision-machined stem design
• Leak-tight sealing performance
• Corrosion-resistant materials
• Long operational lifespan
Quality Assurance and Testing
Every Needle Valve undergoes extensive testing to ensure quality and performance.
Testing includes:
• Hydrostatic Testing
• Pressure Testing
• Leak Testing
• PMI Testing
• Dimensional Inspection
• Material Certification
These procedures ensure compliance with international standards and dependable field performance.
Growing Demand for Precision Flow Control Solutions
As industries continue investing in:
• Industrial Automation
• LNG Infrastructure
• Petrochemical Expansion
• Offshore Energy Projects
• Process Optimization
• Smart Manufacturing Facilities
the demand for high-performance Needle Valves continues to increase globally.
Their ability to deliver precise flow regulation and reliable sealing makes them indispensable in modern industrial systems.
Conclusion
When precise flow control, leak-tight sealing, and operational reliability are essential, Needle Valves remain one of the most effective instrumentation solutions available.
Whether used in oil & gas facilities, power plants, chemical processing units, marine installations, or petrochemical facilities, Needle Valves provide the accuracy and durability required for critical applications.
With advanced engineering, premium materials, and strict quality standards, Mcneil Air Header Needle Valves continue to support industries worldwide with dependable flow control solutions designed for long-term performance.